


Packaging Machine Blog & News
Expert knowledge, equipment selection advice, and technical trends in VFFS, Doypack, Multilane, and Flow Wrap systems.
Engineered with food-grade 316L stainless steel, smart PLC automation, and CIP integration. Designed specifically for high-speed filling accuracy across carbonated, still, hot-fill, and viscous liquid applications.
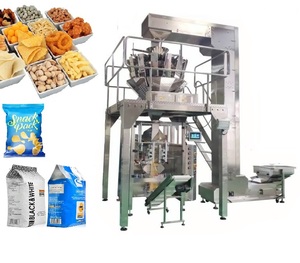
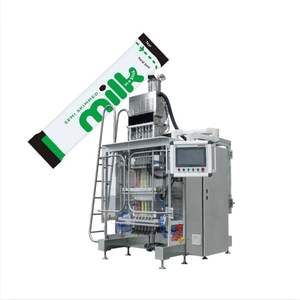
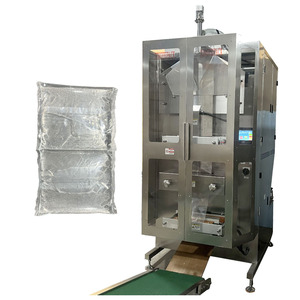
From custom container geometry to high-speed line integration, our engineering teams customize every filling, capping, and labeling component for local compliance and maximum operational efficiency.
Australian Beverage Bottling Industry: Technical Landscape & Market Dynamics
Australia’s beverage manufacturing sector is undergoing a profound transformation driven by shifting consumer preferences toward functional health drinks, premium craft spirits, ready-to-drink (RTD) alcoholic beverages, and ultra-pure mineral waters. As local labor costs continue to rise across major industrial hubs like Sydney, Melbourne, Brisbane, and Perth, automated bottling line efficiency has shifted from a competitive advantage to an absolute operational necessity.
For beverage brand owners, contract packers (co-packers), and micro-breweries in Australia, sourcing robust, high-performance machinery requires a balance of high throughput, rapid format switching, and strict alignment with national safety frameworks. As a premier OEM/ODM beverage bottling machine factory and international exporter, our machinery is specifically engineered to address the distinct geographical, regulatory, and mechanical demands of the Australian market.
Key Australian Market Trends Driving Packaging Automation
Modern Australian beverage plants face unique operating challenges. Understanding these macro trends allows our engineering team to design customized bottling systems that deliver high Information Gain and superior return on investment (ROI):
- Rise of Premium Craft & RTD Beverages: Microbreweries and boutique distillers across Victoria and New South Wales require versatile monoblock filling-capping machines capable of handling both glass bottles and aluminum cans with minimal dissolved oxygen (DO) pick-up.
- Strict APCO Sustainability Mandates: The Australian Packaging Covenant Organisation (APCO) packaging targets mandate higher recyclability and lightweight PET/glass design. Our bottling equipment handles ultralight preforms and 100% rPET bottles without structural crushing.
- Demand for Functional & Cold-Pressed Liquids: Kombucha, cold-brew coffee, juice cleanses, and dairy alternative drinks require aseptic or ultra-clean hot-fill technology paired with laminar flow HEPA air enclosures to guarantee extended shelf life without chemical preservatives.
- High Labor Costs & Industry 4.0 IoT Adoption: Australian plant managers are replacing manual labor with fully automated end-of-line packaging—integrating automated rotary rinsing, precision filling, servo capping, sleeve labeling, and robotic carton palletizing.
Engineering Architecture of Our OEM/ODM Bottling Machines
Our factory utilizes world-class components and robust mechanical design to withstand continuous multi-shift operations in harsh production environments:
- Sanitary Construction: All liquid contact zones are crafted from certified AISI 316L stainless steel with mirror-polished internal surfaces (Ra < 0.4 µm) to prevent bacterial harborage and biofilm build-up.
- Electrical & Control Compliance: Electrical enclosures are fitted with Schneider, Siemens, or Allen-Bradley PLC systems, IP65/IP67 rated wiring, and full compliance with AS/NZS 3000 (Wiring Rules) and AS/NZS 4024 (Safety of Machinery).
- Zero-Drip Diving Nozzles: Bottom-up filling mechanisms equipped with pneumatic anti-drip cut-off valves eliminate neck contamination and maintain uniform fill levels across high-viscosity syrups and foaming liquids.
- Dissolved Oxygen Minimization: Vacuum de-aeration coupled with high-pressure warm water injection (fobbing) or nitrogen gas flushing prior to capping ensures less than 30 PPB DO pickup, safeguarding beverage flavor and shelf stability.
Regional Application Scenarios for Australian Beverage Producers
Our custom-built OEM/ODM bottling machines are deployed across diverse beverage manufacturing sectors nationwide:
Technical and commercial clarity for Australian procurement officers, engineering managers, and plant operations directors.
Why Partner With Our Global Machinery Manufacturing Group
With over two decades of global manufacturing excellence, our state-of-the-art 20,000+ m² production facility houses over 500 skilled mechanical technicians, automation engineers, and quality assurance specialists. We have delivered over 5,000 successful machine installations in more than 80 countries worldwide.
- Full Turnkey Engineering Capability: From raw water treatment (RO systems) and beverage preparation tanks to filling, capping, labeling, shrink wrapping, and robotic palletizing.
- Strict Quality Control & Testing: Every machine undergoes a continuous 72-hour dry and wet Factory Acceptance Test (FAT) using customer-supplied containers and liquid samples before international shipment.
- Transparent Export Management: Complete handling of export documentation, wooden crate packaging treated to ISPM 15 sea-freight standards, and seamless customs coordination for Australian entry.
- Comprehensive Warranty & Service SLA: Backed by a standard 24-month mechanical warranty, lifetime technical assistance, and comprehensive video documentation for operator training.
Ready to Upgrade Your Australian Bottling Plant Efficiency?
Consult with our senior packaging engineers today to get a customized layout design, line capacity calculation, and formal OEM/ODM quotation tailored to your production goals.