


Packaging Machine Blog & News
Expert knowledge, equipment selection advice, and technical trends in VFFS, Doypack, Multilane, and Flow Wrap systems.
Next-Generation Industrial Vacuum Packaging Solutions
In modern commercial food processing, pharmaceutical production, and electronic components manufacturing, establishing absolute control over oxygen degradation, moisture transfer, and microbial proliferation is paramount. As China's premier vacuum packaging machine manufacturer and exporter, SIA Concordia engineers high-vacuum sealing systems that combine precise atmospheric displacement with heavy-duty thermal sealing mechanics. By leveraging high-efficiency rotary vane vacuum pumps, hermetic chamber design, and intelligent PLC touch interface automation, our equipment ensures structural seal integrity, extended product shelf-life, and optimal thermal performance under continuous production environments.
Featured Industrial & Commercial Vacuum Sealing Equipment
Explore our top-rated chamber vacuum sealers, heavy-duty rotary vane vacuum pumps, desktop units, and high-barrier thermoforming packaging machinery designed for export worldwide.
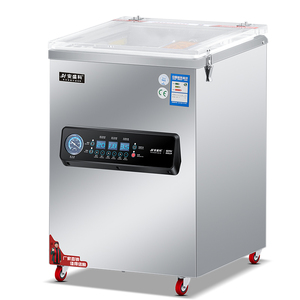
Fully Automatic Industrial/household Chamber Vacuum Sealer Machine
- Dual Sealing Bars for high output
- Heavy-duty 304 Stainless Steel
- Suitable for Meats, Vegetables, Liquids
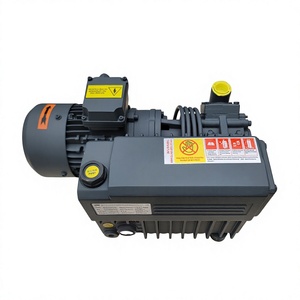
DLT.V0025A Single Stage Oil Sealed Vacuum Pump 25m³/h 1 HP
- High vacuum pumping efficiency
- Ultra-low noise & minimal vibration
- Heavy-cast iron OEM construction
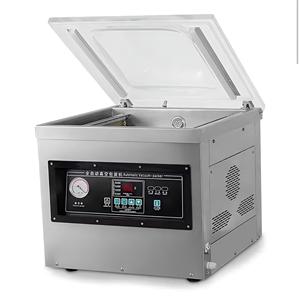
HIPAC DZ300 Automatic Food Vacuum Sealer Commercial Machine
- Microprocessor digital control system
- Precision pressure gauge display
- Compact footprint for processing units
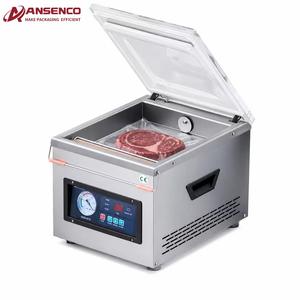
DZ260 Meat Commercial Vacuum Sealer Electric Desktop Unit
- Energy efficient 370W pump drive
- Transparent acrylic dome lid
- Rapid cycle time (10-25 seconds)
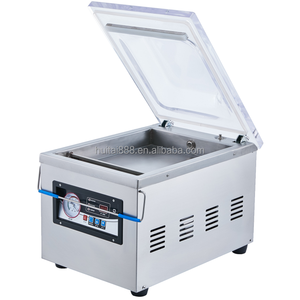
Factory Direct DZ-260 Single Chamber Vacuum Packaging Machine
- Full EU safety & quality compliance
- Pouch sealing length up to 260mm
- Instant thermal impulse sealing mechanism
HIPAC DZ300 Stainless Steel Food Grade Automatic Sealing Machine
- Hygienic washdown design
- Heavy seal pressure for thick foil pouches
- Ideal for fresh meat & seafood export
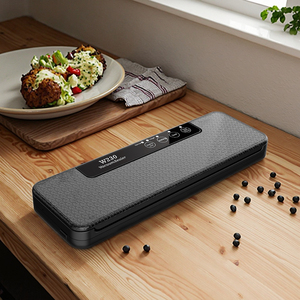
Shineye W-230 Household/Commercial Vacuum Sealing Machine
- One-touch intelligent vacuum & sealing
- Dry / Moist mode customization
- Prevents freezer burn & nutrient loss
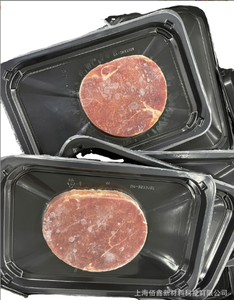
Thermoforming Co-Extrusion High Barrier Vacuum Film Packaging
- Multi-layer EVOH co-extrusion technology
- Exceptional puncture & tear resistance
- Formed specifically for fresh beef & poultry
Industrial Vacuum Packaging Equipment Matrix
Compare structural specifications, pumping capacities, and ideal packaging applications across our core machine categories to determine optimal Total Cost of Ownership (TCO).
| Machine Category | Vacuum Pump Type | Ultimate Pressure | Sealing Length / Bar Count | Throughput Rate | Best Application |
|---|---|---|---|---|---|
| Single Chamber (DZ-260 Series) | Oil-Sealed Rotary Vane (20-25 m³/h) | ≤ 1.0 KPa (10 mbar) | 260 mm / Single Bar | 2-4 cycles / min | Commercial kitchens, deli counters, R&D labs |
| Commercial Double Chamber (DZ-300+) | Dual Rotary Vane Pump (40-60 m³/h) | ≤ 0.2 KPa (2 mbar) | 300 - 500 mm / Dual Bars | 4-8 cycles / min | Meat processing plants, cheese packaging, frozen seafood |
| Thermoforming Continuous Line | High-Capacity Busch Vacuum System (100-300 m³/h) | ≤ 0.1 KPa (1 mbar) | Custom Forming Dies (Flexible/Rigid) | 10-25 cycles / min | High-volume beef slaughterhouses, medical device packaging |
| External Suction Vacuum Sealer | Dry Diaphragm / Piston Pump | ≤ 80 KPa | 300 - 400 mm / Single Bar | 1-2 cycles / min | Dry electronics, grain sachets, home storage |
Global Procurement & Technology Trends in Vacuum Packaging
As environmental regulations tighten and labor costs rise worldwide, the industrial vacuum packaging market is undergoing three major technological transformations.
1. MAP (Modified Atmosphere Packaging) Integration
Simple air extraction is increasingly replaced by precision gas flushing (N₂, CO₂, O₂ blends). MAP vacuum sealers preserve red meat color while inhibiting anaerobic bacteria growth without chemical preservatives.
2. Smart PLC & Industry 4.0 Telematics
Modern B2B buyers mandate IoT-enabled PLC touchscreens capable of logging real-time vacuum pressure curves, thermal seal temperatures, and maintenance diagnostics directly to ERP systems via Modbus/Ethernet.
3. Sustainable Mono-Material Pouch Sealing
Transitioning away from non-recyclable multi-material laminates toward mono-PE and mono-PP recyclable films requires precise digital impulse temperature control to prevent seal burnout while maintaining vacuum hermeticity.
Why SIA Concordia is China's Trusted Vacuum Packaging Exporter
Under strict ISO 9001:2015 quality control management, our manufacturing facilities adhere to European safety standards, delivering verified structural integrity for international importers.
20,000 m² Manufacturing Facility
Equipped with high-precision CNC laser cutters, robotic welding cells, and automated test benches to ensure every vacuum chamber guarantees exact dimensional tolerance and zero structural vacuum leaks.
Full R&D & Custom Engineering
Our team of 500+ engineers provides bespoke OEM/ODM machinery modifications, including custom chamber depths, specialized conveyor integration, gas injection modules, and custom voltage configurations (110V-480V, 50/60Hz).
Global Technical Support & Spare Parts
Serving clients across 80+ countries, SIA Concordia maintains strategic spare parts depots and rapid remote video diagnostics to guarantee maximum uptime for continuous food processing operations.
Industrial Vacuum Packaging Procurement FAQ
Answers to essential technical and commercial questions evaluated by enterprise buyers during machine sourcing.
Q1: How do I determine the correct vacuum pump size for my processing volume?
Pumping speed (measured in m³/h) determines chamber evacuation speed. For low-volume commercial applications (DZ-260), a 20 m³/h pump suffices for 15-20 second cycles. For heavy industrial lines requiring under 10-second evacuation, choose dual-stage oil-sealed pumps rated at 60 m³/h to 100 m³/h to maintain rapid production tempo.
Q2: What is the difference between single chamber and double chamber vacuum sealers?
Single chamber machines (like the DZ-260/DZ-300) feature one lid and one chamber cavity, ideal for small-to-medium batches. Double chamber machines feature a swinging lid over two separate chambers; while one chamber is undergoing vacuum displacement and thermal sealing, the operator loads bags into the second chamber, effectively doubling throughput efficiency.
Q3: Can these machines package liquids, sauces, or wet soups?
Yes. Chamber vacuum sealers equalize pressure inside the entire enclosure during air removal. Unlike external suction sealers which pull liquids out of the pouch, chamber sealers keep liquids inside the bag during evacuation. For high-temp liquid products, custom inclined plates are recommended to keep pouch openings elevated above the seal bar line.
Q4: How does vacuum level affect food shelf life?
Lowering internal oxygen content below 0.5% halts aerobic bacterial growth, oxidative rancidity of fats, and enzyme degradation. Combined with proper cold-chain refrigeration, vacuum packaging extends raw meat shelf life from 3-5 days to 21-45 days depending on barrier film density.
Q5: What routine maintenance is required for rotary vane vacuum pumps?
Primary routine maintenance involves inspecting oil clarity through the sight glass every 50 operating hours, performing oil changes every 500 hours (or sooner if packaging high-moisture items), and regularly replacing the internal exhaust oil mist separator filter to prevent vacuum pump thermal overload.
Q6: Are SIA Concordia vacuum packaging machines CE and ISO compliant for import into the EU and US?
Yes. All export machinery complies strictly with Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and carries CE certification. Stainless steel contact components conform to FDA food-contact standards, ensuring seamless customs clearance for North American and European importers.
Request Custom Quotation & Technical Specifications
Consult with our senior application engineers to receive tailored packaging line recommendations, factory-direct wholesale pricing, and complete digital equipment catalogs.
Get Catalog